Cycle: All Milling cycles
Definition
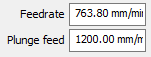
Plunge Feedrate is the speed at which the tool moves in the Z axis.
|
The purpose of this parameter is to provide an intermediate speed for plunge because GO2cam programs a plunge with a feedrate; but the work feedrate is slow, so the Plunge Feedrate value allows to speed up the plunge motion and then returning back to the feedrate value. The Plunge Feedrate is used during Z-axis plunging movements when entering a machining level. In operations involving multiple Z levels, the tool may perform this movement repeatedly throughout the toolpath. The Plunge Feedrate should not be confused with the rapid movement speed. A plunge is a controlled Z-axis feed movement and therefore its duration depends directly on the configured plunge feedrate. |
|
|
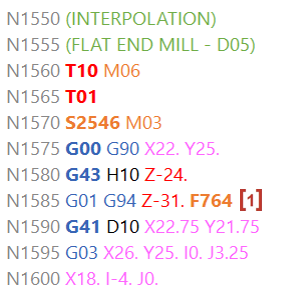
Plunge Feedrate = 0 |
The plunge is done with the work feedrate [1]. |
|
|
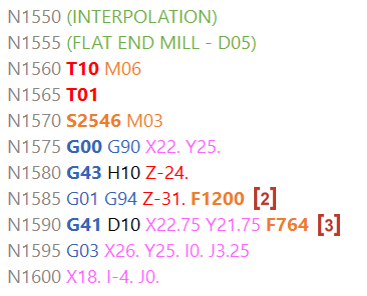
Plunge Feedrate = 1200 |
The tool plunges with the value 1200 [2] then start working by modifying the feedrate back to the standard value [3]. |
|
Important: The Plunge Feedrate can have a significant impact on machining time, particularly when the tool performs multiple Z-level passes. A very low Plunge Feedrate can considerably increase the total machining time because the tool must move at this speed each time it plunges to the next machining level.
|